When B2B buyers evaluate sponge suppliers, the numbers on a quote sheet are rarely the primary concern. What truly matters is: "How is this sponge made?" From raw material sourcing and formula formulation to process control and testing—each answer determines whether the final product passes end-market inspection.
This article breaks down every step of wood pulp sponge production, from cellulose raw materials to finished goods. Whether you are a procurement manager, product manager, or quality control lead, this guide provides a systematic evaluation framework to help you know exactly what to look for and what to ask during factory audits or price comparisons.
## 1. Raw Materials: The Foundation of Performance
The core raw material for wood pulp sponges is **wood pulp cellulose**, typically derived from softwoods (e.g., pine, spruce) or hardwoods (e.g., birch, eucalyptus). Variations in cellulose chain length and degree of polymerization across different wood species directly impact the final product's absorbency, softness, and durability.
### 1.1 Cellulose Extraction Process
Wood pulp cellulose is extracted from logs via chemical or mechanical pulping:
- **Chemical Pulping (Kraft Process)**: Dissolves lignin using sodium hydroxide and sodium sulfide under high temperature and pressure, preserving cellulose. This method yields fibers with high purity and strength, making it the preferred choice for premium wood pulp sponges.
- **Mechanical Pulping**: Separates fibers through physical grinding, retaining more lignin. While cost-effective, the resulting fiber quality is slightly inferior.
- **Dissolving Pulp**: Offers the highest cellulose purity, with α-cellulose content ≥90%, specifically designed for manufacturing regenerated cellulose products.
### 1.2 Key Raw Material Specifications
| Parameter | Premium Standard | Impact |
|------|----------|------|
| α-Cellulose Content | ≥88% | Determines water absorption ratio and softness |
| Degree of Polymerization (DP) | 500-800 | Affects mechanical strength and durability |
| Brightness | ≥85% ISO | Influences finished appearance and dyeing results |
| Ash Content | ≤0.5% | High ash indicates impurities, affecting product purity |

## 2. Formulation: The Code for Customized Performance
Once qualified cellulose is secured, the next step is **formulation design**. Properties such as water absorption speed, retention capacity, softness, resilience, and antimicrobial efficacy can all be customized by adjusting the formula.
### 2.1 Basic Formula Composition
A typical wood pulp sponge formula includes the following components:
- **Wood Pulp Cellulose** (60-75%): Primary structural material
- **Cross-linking Agent** (3-8%): Such as epichlorohydrin (ECH) or citric acid, forming chemical bonds between cellulose molecules to enhance wet strength
- **Blowing Agent** (2-5%): Such as sodium bicarbonate or azodicarbonamide, generating gas during heating to create a porous structure
- **Plasticizer** (5-10%): Such as glycerin or polyethylene glycol, adjusting softness and hand feel
- **Functional Additives** (1-5%): Antimicrobials, flame retardants, pigments, etc.
### 2.2 Customization Strategies
Performance requirements vary significantly across application scenarios:
| Application Scenario | Core Performance Needs | Formula Adjustment Direction |
|----------|------------|-------------|
| Kitchen Cleaning | High absorbency, strong oil removal | Increase cellulose ratio, add lipophilic groups |
| Automotive Detailing | High softness, paint-safe | Increase plasticizer, reduce cross-link density |
| Personal Care | Ultimate softness, antimicrobial | Add silver ion antimicrobial agents, optimize foaming process |
| Industrial Wiping | High abrasion resistance, chemical corrosion resistance | Increase cross-linking, add corrosion-resistant additives |
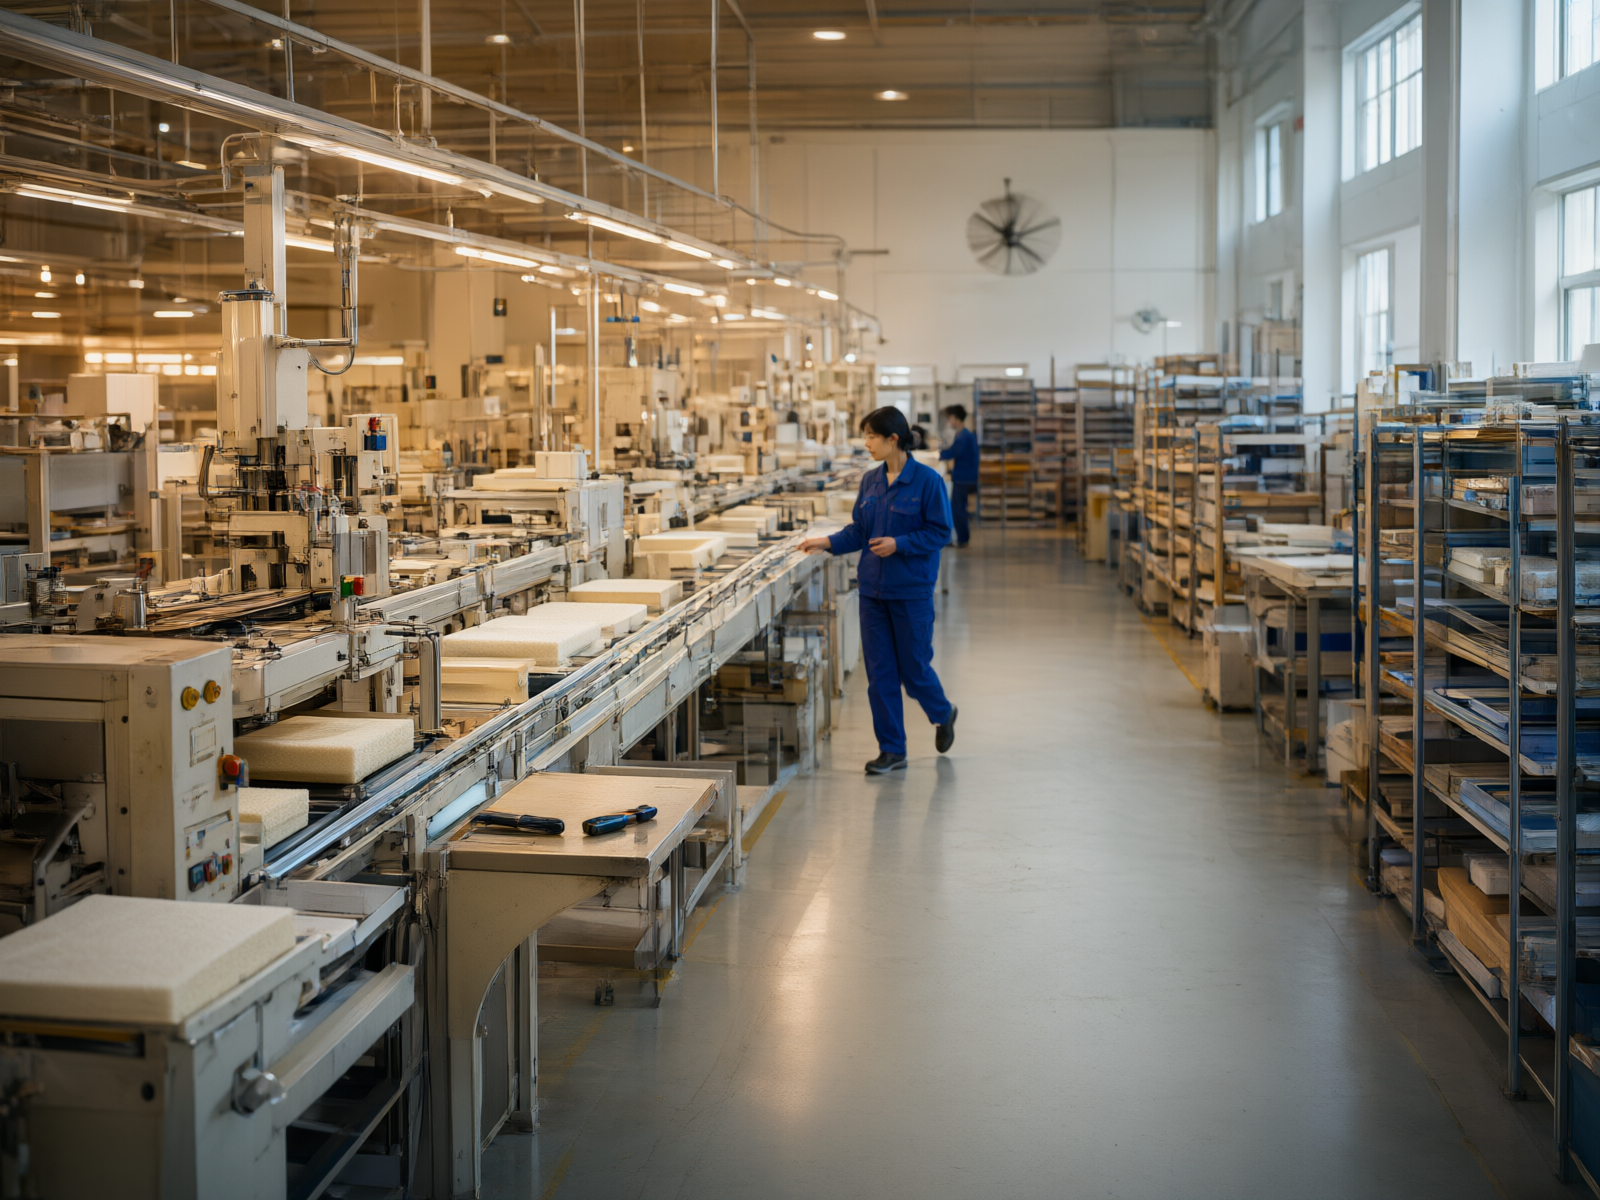
## 3. Production Process: Transforming Slurry into Finished Goods
With the formula finalized, production begins. Wood pulp sponge manufacturing primarily involves these steps:
### 3.1 Slurry Preparation
Mix wood pulp cellulose with deionized water at a specific ratio and beat the mixture in a high-shear mixer to ensure thorough fiber dispersion. Beating degree (°SR) is a critical control parameter:
- **Low Beating Degree (20-30°SR)**: Longer fibers yield high-strength sponges but rougher surfaces
- **Medium Beating Degree (30-45°SR)**: Balanced performance, suitable for most products
- **High Beating Degree (45-60°SR)**: Short, fine fibers create smooth surfaces but slightly lower strength
### 3.2 Mixing and Blending
Add cross-linking agents, blowing agents, and plasticizers to the slurry according to the formula ratio. Mix uniformly in a temperature-controlled tank. Mixing temperature is typically maintained at 25-35°C to prevent premature decomposition of the blowing agent.
### 3.3 Molding and Foaming
Inject the mixed slurry into molds and transfer to a foaming furnace. The foaming process occurs in two stages:
1. **Pre-foaming** (60-80°C, 10-15 minutes): Blowing agent begins decomposing; slurry volume expands 1.5-2 times
2. **Main Foaming and Curing** (120-160°C, 20-40 minutes): Blowing agent fully decomposes while cross-linking reactions proceed simultaneously, setting the sponge structure

### 3.4 Post-Treatment
After foaming and curing, the sponge undergoes the following post-processing steps:
- **Washing**: Removes residual chemicals and unreacted monomers
- **Dewatering**: Removes excess moisture via centrifugation or pressing
- **Drying**: Dries in an oven at 60-80°C until moisture content is ≤10%
- **Cutting**: Trims to customer-specified dimensions and shapes
- **Surface Treatment**: Includes embossing, printing, coating, etc.
## 4. Quality Control: Let Data Speak
Quality control distinguishes professional manufacturers from workshops. A qualified wood pulp sponge producer must establish a comprehensive testing system across the following dimensions:
### 4.1 Physical Property Testing
| Test Item | Test Standard | Acceptable Range |
|----------|----------|----------|
| Water Absorption Ratio | GB/T 461.2 | ≥8 times self-weight |
| Water Retention Rate | ISO 535 | ≥60% |
| Resilience | ASTM D3574 | ≥85% (after 50% compression) |
| Tensile Strength | GB/T 1040 | ≥0.3 MPa (wet state) |
| Tear Strength | ISO 13937 | ≥2 N/mm |
### 4.2 Chemical Safety Testing
- **Formaldehyde Content**: ≤75 mg/kg (compliant with GB 18401 Class B standard)
- **Heavy Metal Content**: Lead, cadmium, mercury, and hexavalent chromium all ≤100 ppm (RoHS compliant)
- **pH Value**: 6.0-8.0 (neutral, non-irritating to skin)
- **Migratable Fluorescent Whitening Agents**: Not detectable
### 4.3 Microbiological Testing
- **Total Bacterial Count**: ≤1000 CFU/g
- **Mold and Yeast Count**: ≤100 CFU/g
- **Coliform Bacteria**: Not detectable
- **Staphylococcus aureus**: Not detectable

## 5. Customization Capabilities: From Standard Products to Tailored Solutions
For B2B buyers, a supplier's **customization capabilities** often outweigh standard product pricing. A capable wood pulp sponge manufacturer should offer customization across the following dimensions:
### 5.1 Size and Shape Customization
- Standard sizes: 110×70×40mm, 150×100×50mm, etc.
- Custom shapes: Circles, ovals, waves, or client-specified designs
- Thickness range: 5mm-100mm
### 5.2 Performance Customization
- Water absorption ratio: Adjustable from 5 to 15 times
- Softness: Shore hardness adjustable from 10 to 50A
- Density: Adjustable from 80 to 300 kg/m³
- Color: Any Pantone color code available
### 5.3 Packaging and Branding Customization
- OPP bags, blister packs, color boxes
- Customer logo printing (screen printing, heat transfer, laser engraving)
- Custom hangtags, instruction manuals, barcodes

## 6. Procurement Decision Guide: How to Evaluate Suppliers
Based on this end-to-end breakdown, B2B buyers evaluating wood pulp sponge suppliers should focus on the following key points:
1. **Raw Material Traceability**: Can they provide origin certificates and test reports for cellulose?
2. **Formula R&D Capability**: Do they have an independent R&D lab? Can they customize formulas based on needs?
3. **Production Process Control**: Is there a complete SOP and process documentation? Are critical parameters monitored online?
4. **Quality Testing System**: Are they ISO 9001 certified? Is testing equipment comprehensive?
5. **Customization Response Time**: How long does sampling to delivery take? What is the minimum order quantity?
6. **Environmental Compliance**: Are they FSC certified? Do wastewater and exhaust treatment systems meet standards?
---
*What appears to be a simple wood pulp sponge is actually a sophisticated integration of cellulose science, polymer chemistry, and precision manufacturing. Choosing a supplier is fundamentally about selecting a complete quality assurance system. We hope this guide helps you make more informed, professional decisions in your next procurement.*
Return news list
Technical Sharing2026-10-01
The Journey of a Wood Pulp Sponge: From Cellulose Raw Material to Customized Product
When B2B buyers evaluate sponge suppliers, the key question isn't just about price—it's about how the sponge is made. Where do raw materials come from? How are formulas developed? What controls govern the production process? How are quality checks performed? The answers to each of these determine whether the final product passes end-market validation.

Previous
Bath Sponge | Soft & Skin-Friendly, Elevate Your Shower Experience
2026-08-24
Next
This is the last one.
Want to learn more about the sponge products industry?
Contact our expert team